Workplace accidents do not happen because safety regulations are missing; they happen when risks are not detected in time. This was the challenge faced by a global building materials group operating two manufacturing plants in Vietnam, despite having comprehensive CCTV coverage across both facilities. VTI deployed AI-powered behavior recognition across more than 40 cameras to automatically detect PPE (Personal Protective Equipment) violations, restricted-area intrusion, forklift–pedestrian collision risks, and other unsafe behaviors. The solution was integrated into a centralized workplace safety monitoring portal, together with FaceX facial recognition-based attendance management. This project demonstrates how technology can transform existing CCTV infrastructure into a proactive safety layer that continuously monitors operations 24/7.
Company Background
Company Overview
The client is a leading multinational group specializing in building materials and advanced industrial solutions, with hundreds of years of operating history and a global presence. In Vietnam, the group operates two large-scale manufacturing plants, with hundreds of employees working across multiple production shifts. The operating environment involves complex safety risks associated with forklifts, heavy-duty warehouses, and restricted-access areas.
As a global enterprise, the company already maintains stringent EHS (Environment, Health & Safety) standards. Workplace safety training is conducted regularly, comprehensive safety regulations are in place, and CCTV cameras provide extensive coverage across the manufacturing facilities. Despite these measures, safety incidents continued to occur.
Business Challenges
During the assessment of the existing operations, the VTI team identified a critical gap: CCTV cameras were available throughout the facilities, but there were not enough resources to continuously monitor all camera feeds 24/7. A worker entering a restricted area, a forklift operating too close to a pedestrian, or an employee looking at a mobile phone while walking could all create significant safety risks. Such risks could easily go unnoticed until after an incident occurred.
The company needed to optimize its safety monitoring process not only by recording incidents after they occurred, but by detecting unsafe behaviors and generating real-time alerts directly from the production environment. Therefore, the Group’s leadership team identified two key requirements for VTI:
- First, an automated system capable of detecting unsafe behaviors through the existing CCTV infrastructure and generating immediate alerts.
- Second, a centralized management portal capable of processing all behavior-related alerts while also managing employee information and daily attendance logs, replacing manual processes that were prone to errors and lacked transparency across several hundred employees working multiple shifts at multiple plants.
Technical Challenges
Before designing the solution, the VTI team conducted on-site assessments at both manufacturing plants and determined that the requirements could not be addressed effectively with a generic, off-the-shelf AI model.
Each facility has its own layout, pedestrian and vehicle flows, lighting conditions, and EHS risk scenarios. A single general-purpose model would not be sufficient to accurately handle specific use cases such as:
- Recognizing the correct PPE required under the group’s safety standards
- Distinguishing between a person standing near a forklift and a person operating within an authorized area
- Detecting workers climbing stairs without holding the handrail
In addition, integrating real-time alert streams from more than 40 cameras into a single portal while simultaneously supporting safety monitoring, employee management, and facial recognition-based attendance required a custom software architecture designed around the customer’s actual operational requirements.
VTI’s AI-Powered Workplace Safety Monitoring Solution
AI Behavior Recognition Across 40+ CCTV Cameras
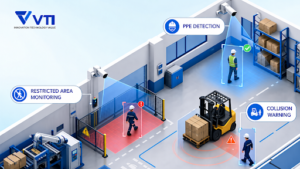
VTI developed and trained independent AI Computer Vision models for each safety monitoring use case and deployed them directly on the customer’s existing CCTV infrastructure without requiring hardware replacement. More than 40 cameras across the two manufacturing plants were integrated into the intelligent monitoring system, covering five key behavior-recognition use cases:
- PPE Detection: The system automatically identifies workers who are not wearing the required PPE, including safety helmets, gloves, and reflective vests. Whenever a violation is detected, an alert is immediately sent to the Portal and via email to the EHS team and relevant plant managers.
- Mobile Phone Use While Walking: Using a mobile phone while walking through production areas can create a significant accident risk and is difficult to monitor consistently through manual observation. The AI safety monitoring model detects and records each violation event in real time.
- Restricted-Area Intrusion Detection at the SLP Warehouse: The SLP warehouse contains strictly controlled restricted areas. The system automatically detects and generates an alert whenever an unauthorized person enters a restricted zone, regardless of the time of day.
- Forklift–Pedestrian Collision Risk Detection: Forklift-related incidents are among the key safety risks in manufacturing environments. By simultaneously detecting active forklifts and pedestrians within the same defined spatial zone, the AI model can generate an immediate alert when a potential collision risk is identified.
- Stair Climbing Without Handrail Use: This is a site-specific use case at the HPC plant, where industrial staircases are subject to mandatory handrail-use requirements. A dedicated model was trained to detect this specific unsafe behavior with high accuracy.
Centralized Management Portal with FaceX Attendance
Alongside the behavior monitoring system, VTI developed a centralized management portal serving both manufacturing plants with three core functions:
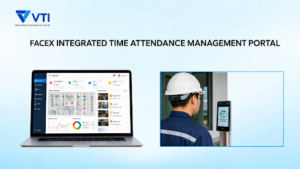
Facial Recognition-Based Attendance with FaceX: FaceX attendance management was deployed with a facial registration module directly integrated into the Portal, replacing the customer’s previous manual or card-based attendance processes. Recognition data is synchronized in real time to support automated working-hour calculation and shift management.
Employee Management and Shift Configuration: The Portal consolidates employee profiles, shift assignments, and daily attendance logs within a single interface. Management can configure shifts flexibly, monitor attendance, and retrieve historical records without switching between multiple standalone systems.
EHS Alert Management Center: All safety violation events captured by the 40+ cameras are consolidated into a single dashboard on the Portal, together with supporting images, timestamps, and camera locations. Alerts are also automatically distributed via email to the appropriate management levels based on predefined access and notification rules.
Implementation Results
Following deployment across the manufacturing plants, several notable improvements were observed:
- Reduced PPE violations and restricted-area intrusions since the system created an immediate feedback loop: a violation occurs → an alert is generated → management responds promptly → employee behavior gradually improves through continuous monitoring and evidence-based follow-up.
- EHS teams no longer need to spend hours manually reviewing footage after incidents. Instead, they have access to a complete, searchable alert log that can be retrieved and reported on a weekly or monthly basis for group management.
- Attendance and workforce management were transformed from fragmented manual processes into a centralized digital workflow, reducing errors, saving administrative time, and improving data transparency.
- Over time, employee compliance improved as workers became more aware that safety violations were consistently detected, recorded, and addressed.
Key takeaway from the project
This project demonstrates an important reality of digital transformation in manufacturing: hardware infrastructure alone is not enough. What is needed is an intelligent layer that can turn camera data into actionable safety insights.
For a multinational enterprise operating under global EHS standards, the solution could not simply be an off-the-shelf product. The value of the project lies in VTI’s ability to train AI models for site-specific scenarios, deploy them without replacing the existing infrastructure, and integrate everything into a unified operational system from on-site cameras and real-time alerts to email notifications for management.
If your business operates a manufacturing facility equipped with a CCTV system, but workplace safety challenges have not yet been fully addressed through technology, VTI is ready to provide consultation and assess your current operations.
Contact us today to explore AI-powered behavior recognition and smart attendance solutions tailored to your factory’s operational needs.